JI'NAN, China, Sept. 17 — GenScript Biotech Corporation (HK.1548), a world-leading life science R&D and manufacturing service provider, announced today that its subsidiary, Bestzyme Biotech, has completed the construction of an automated, intelligent sweet protein production line in Ji'nan, China. This marks the official completion of the world's first commercial production line specifically designed for sweet proteins. It also signifies a strategic leap in Bestzyme's industrial manufacturing capabilities, making it the first company to achieve full supply chain integration and the global leader with end-to-end, proprietary mass-production capacity in the synthetic biology sweet protein sector.
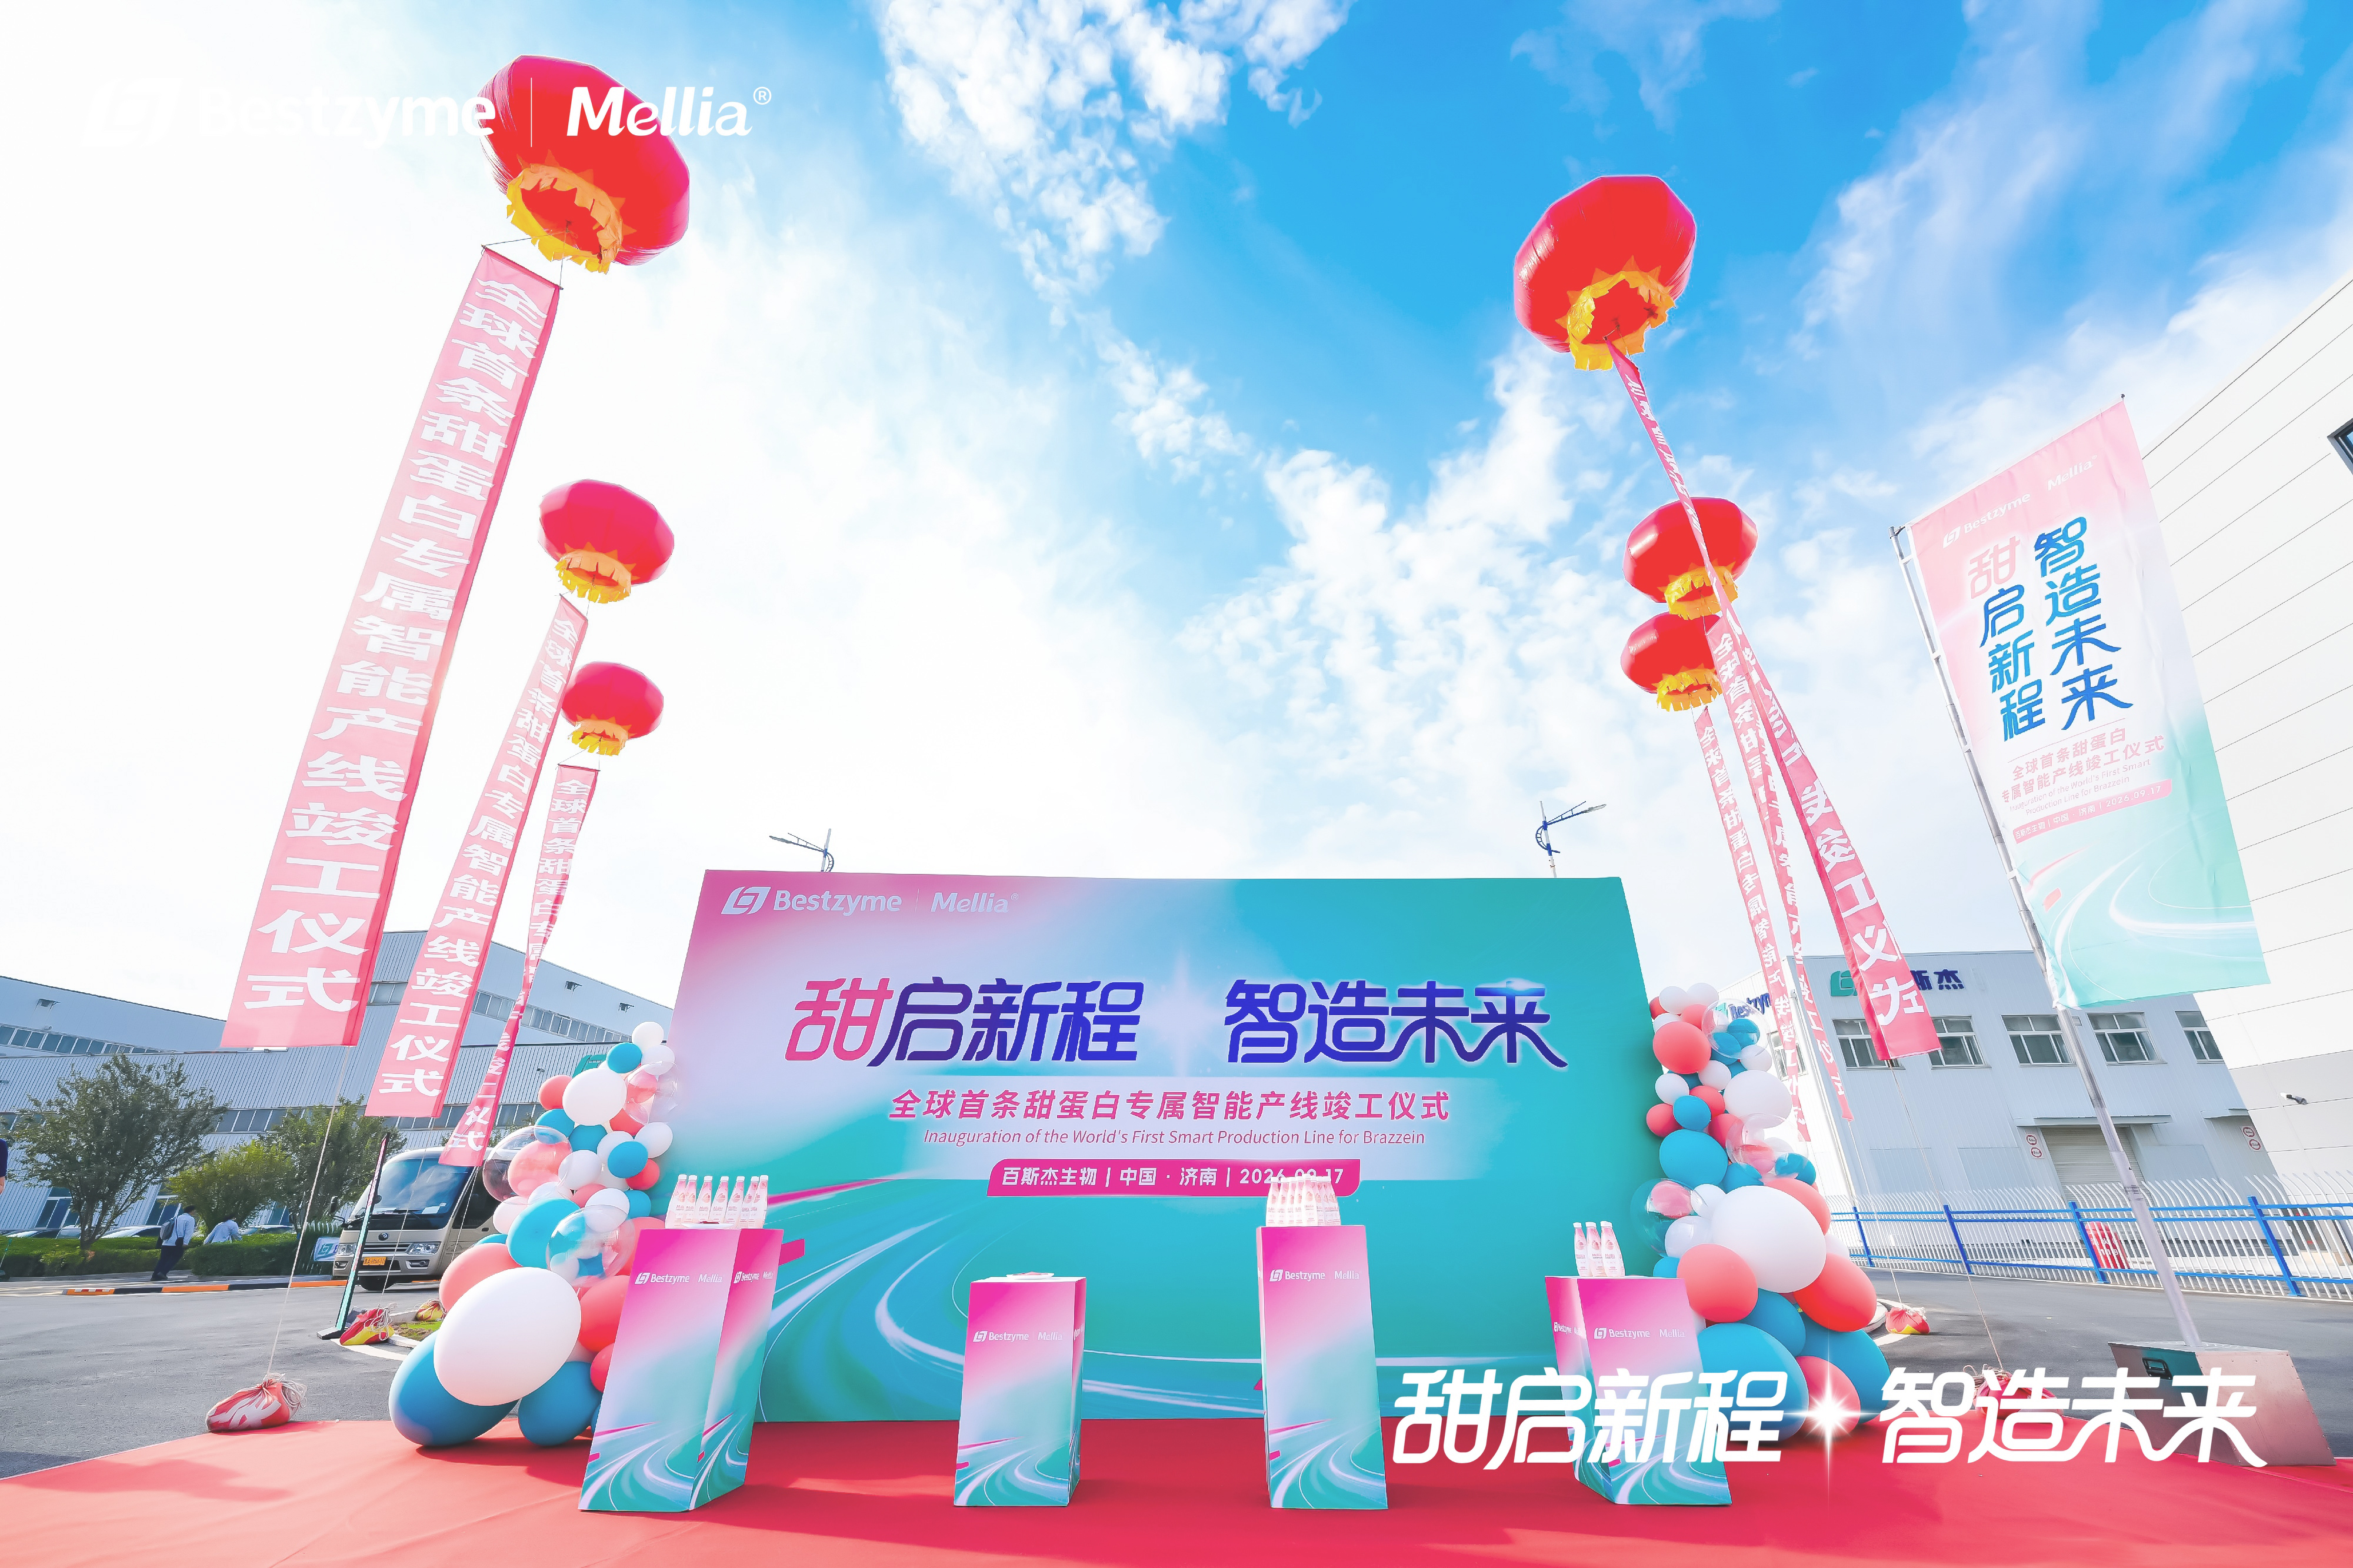
The completion of this automated line brings Mellia®—Bestzyme's Brazzein sweet protein and the first domestic product of its kind to receive GRAS recognition from the U.S. FDA—into a new phase of industrial-scale mass production. This milestone resolves long-standing industry bottlenecks such as low yield, batch instability, and prohibitive costs. It also underscores China's leading position in high-value synthetic biology manufacturing, engineering delivery, and global supply chain compliance.
Ms. Yu Zhang, Vice President of Market and Business Development at Bestzyme, introduced the core product manufactured on this line: Bestzyme Mellia® Brazzein. Originating from the West African wild plant Oubli, Brazzein is a natural sweet protein with a sweetness thousands of times higher than sucrose. It produces virtually no calories and has negligible impact on blood sugar, serving as a next-generation healthy sugar-reduction solution. Leveraging synthetic biology and high-density precision fermentation, Bestzyme has successfully commercialized this scarce natural protein to build a robust supply chain foundation for the global food and beverage industry.
Dr. Aixi Bai, General Manager of Bestzyme, highlighted that the global food and beverage industry is undergoing a profound wellness transformation. Reducing sugar is not only a regulatory trend but also a strong consumer demand for healthier lifestyles. However, traditional alternative sweeteners face limitations in flavor profiles, consumer acceptance, and application versatility, often leaving undesirable bitter or metallic aftertastes.
"The true challenge of sugar reduction is never simply removing sugar, but perfectly replicating the pure, full-bodied, and natural taste of sucrose while eliminating calories and metabolic burden," said Dr. Bai. "Bestzyme Mellia® sweet protein is the critical missing piece that satisfies consumers' desire for authentic sweetness. Under our brand proposition 'Make Sweetness Complete,' we are dedicated to providing global partners with revolutionary solutions that balance health, safety, and exceptional flavor. The inauguration of our Ji'nan production line is both a realization of our core R&D achievements and a commitment to delivering a stable, compliant, and high-quality commercial product to the global market."
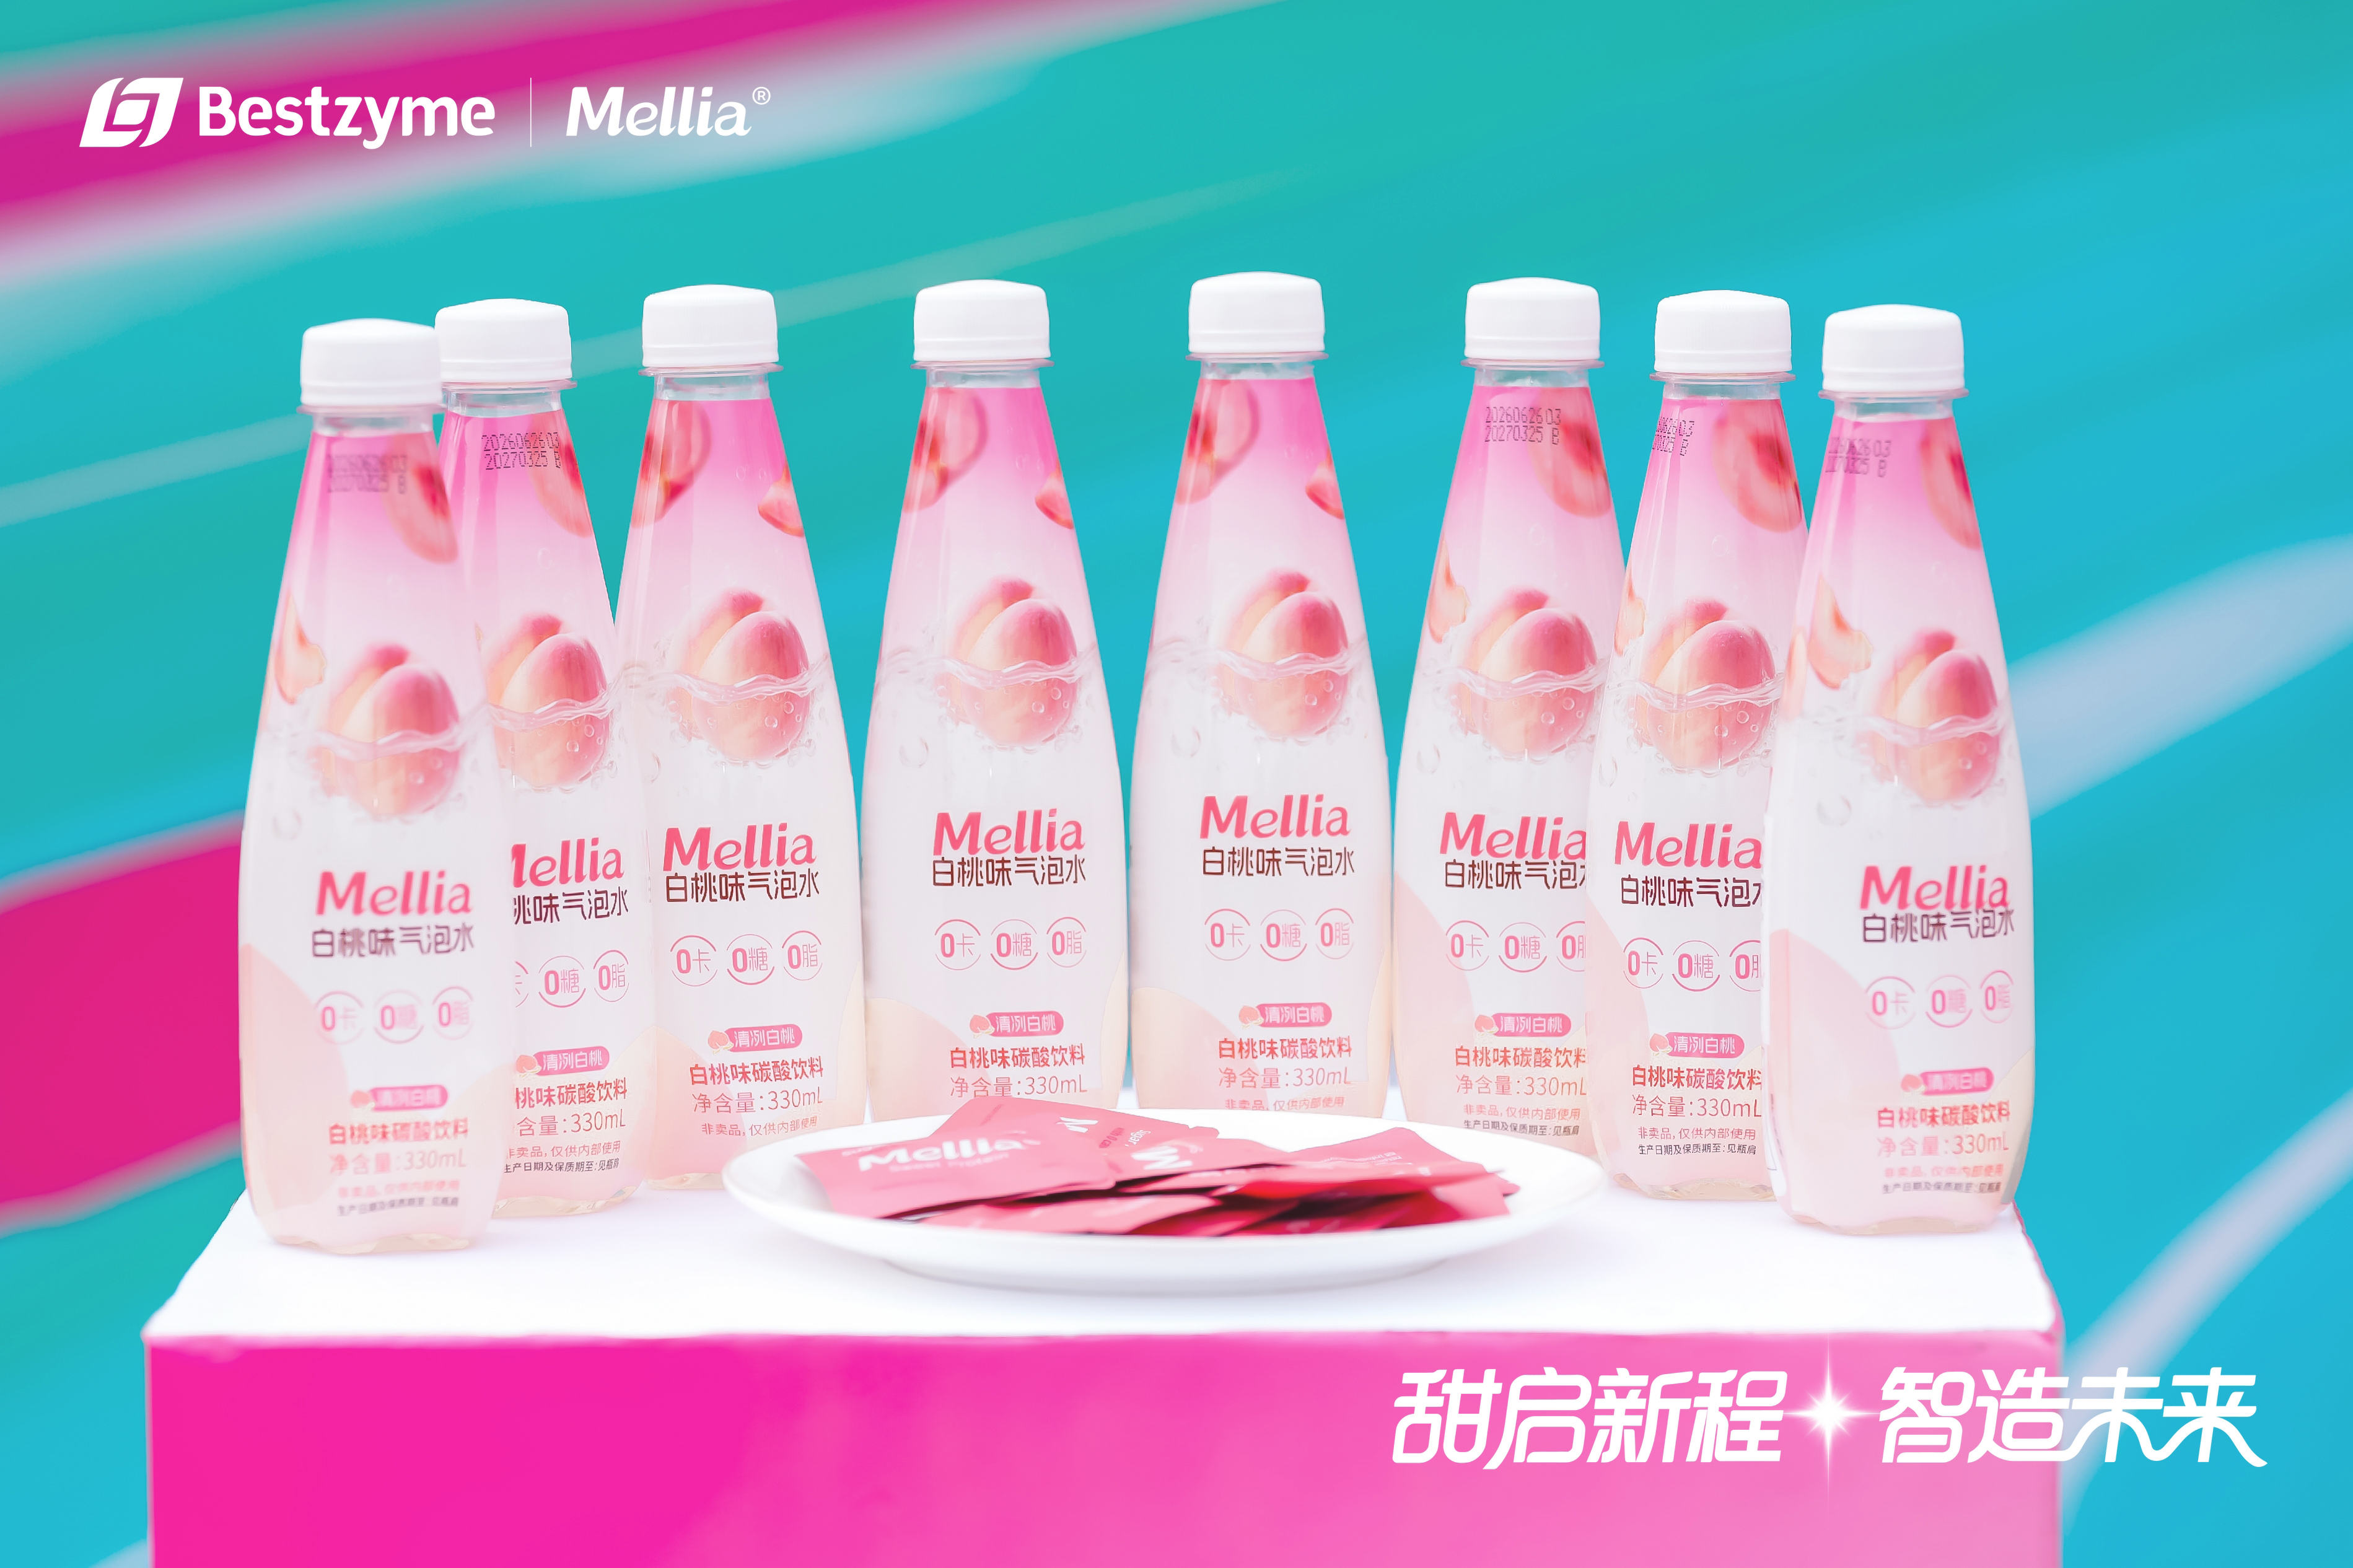
End-consumer products showcased on-site, including sugar-free sparkling water and sugar-free pressed candies developed with Mellia® sweet protein
For the synthetic biology industry, R&D forms the foundation, but fermentation scaling and engineering implementation determine ultimate success. Sweet proteins have long remained confined to laboratory or pilot-scale samples due to low expression levels in host organisms and extreme purification difficulties, driving up costs. Drawing on more than a decade of experience in industrial enzymes and biocatalytic manufacturing, Bestzyme overcame critical scaling hurdles, including high-yield strain development, high-density fermentation, and high-purity crystallization separation.
The newly constructed 5,000-square-meter facility in Ji'nan features rare end-to-end automated capabilities spanning fermentation, purification, and freeze-drying. Equipped with intelligent fermentation control systems and cleanrooms compliant with international standards, the facility ensures high stability and premium quality across mass production.
Once fully operational, the annual capacity for Mellia® sweet protein products will reach over 100 metric tons. Based on the sweetness intensity of high-purity Brazzein, this capacity is equivalent to supplying the sweetness of 300,000 tons of sucrose per year, overcoming the industry barrier where sweet proteins were conceptually appealing but unavailable for bulk procurement. Through continuous strain iteration and process optimization, Bestzyme plans to double its capacity within the next two years, fully equipping the facility for stable, large-scale supply to top-tier global food and beverage manufacturers.
Officials from the Shanghe Economic Development Zone in Shandong who attended the ceremony commended the project, stating that the line reflects Bestzyme's commitment to independent innovation and highlights the region's progress in high-tech biomanufacturing. By filling a global gap in industrial-grade sweet protein manufacturing, the facility demonstrates China's growing capabilities in advanced synthetic biology.
As consumer preferences shift toward cleaner tastes and superior sensory experiences, food and beverage companies are transitioning from buying single raw ingredients to seeking comprehensive application solutions.
Mr. Hua Mao, Senior Partner and Managing Director of Frost & Sullivan Greater China, shared industry insights during the event. He noted that supplying bulk powder is no longer enough to solve complex flavor challenges. As functional macromolecules, sweet proteins exhibit varying sweetness release curves and flavor interactions across different matrices like carbonated drinks, plant-based dairy, and confectionery. Solution providers with full-stack application R&D and formulation guidance are best positioned to build strong competitive moats.
The launch of the Ji'nan base signifies Bestzyme's transformation into a Full-Value-Chain Sweetness Partner. Backed by an application science team and sensory evaluation platform, Bestzyme offers an integrated ecosystem: Strain R&D→Scalable Mass Production→Custom Formulation Blending→Global Regulatory Support.
This setup enables customized sweetness blending and flavor modification solutions tailored to client product lines, shortening the time-to-market cycle for end products by several months.
Following the ceremony, guests toured the intelligent workshop and application laboratory. Sampling products such as sugar-free sparkling water and sugar-free pressed candies made with Mellia®, attendees praised the sweet protein for delivering a clean, rich sweetness close to sucrose without the lingering bitterness of traditional sugar substitutes.
Regulatory compliance is a critical barrier to entering global markets for high-value synthetic biology products. Alongside scaling production, Bestzyme has actively pursued domestic and international regulatory approvals.
United States: In April 2025, Mellia® received a "No Questions Letter" from the U.S. FDA, officially securing FDA-GRAS status. It became the first domestic Brazzein sweet protein to earn this recognition, establishing a solid regulatory base for international markets.
China: In March 2025, Bestzyme submitted an application for a new food additive variety, which was formally accepted by the National Health Commission (NHC), making Bestzyme the first company in China to initiate this process.
From technological R&D to scale manufacturing, and from product application to global regulatory compliance, Bestzyme is building a complete commercial ecosystem for sweet proteins. The completion of the Ji'nan smart production line enhances supply reliability, providing new possibilities for the global food and beverage sector as it explores healthier sugar-reduction pathways.
© Bestzyme. All rights reserved.